-

Accelerated ejectors
There are many ways to achieve an accelerated ejector pin movement, but for its simplicity and reliability we often turn to the Strack Z141 acceleration rocker. The rocker pin is pushed forward an extra 7,6mm when the ejector set has reached its forward most position. This is normally enough to get a tricky part to…
-
Conformal cooling with TempFlex
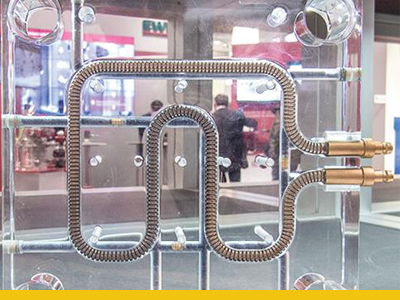
A new solution for conformal cooling is available in the HASCO TempFlex. [ut_blockquote_left] No deep-hole boring and plugging gives cost reduction for manufacturing mould plates. [/ut_blockquote_left] The flexible metal-braided hose allows fast and simple assembly and interchangeability, and is adaptable to most groove patterns. Made of stainless-steel corrugated tubing, they are laid into channels milled…
-

CoolCross for improved cooling
A recent product development from HASCO, the Z99 CoolCross is making routing of cooling channels easier and more efficient. [ut_blockquote_right] Reduce plate thickness and improve cooling [/ut_blockquote_right] With this new system, it is possible to have cooling channels crossing each other on the same plane in a flexible and inexpensive manner. The CoolCross injection mold…
-

Draft angles for VDI surfaces
VDI Ra Rz, DA-PA DA-PC DA-ABS 12 0,40 1,5 0 1,0 0,5 15 0,56 2,4 0,5 1,0 0,5 18 0,80 3,3 0,5 1,0 0,5 21 1,12 4,7 0,5 1,0 0,5 24 1,60 6,5 0,5 1,5 1,0 27 2,24 10,5 1,0 2,0 1,5 30 3,15 12,5 1,5 2,0 2,0 33 4,50 17,5 2,0 3,0 2,5…
-

Electric valve gate systems
At The Tool Hub we constantly see new technology in the industry and one that is now adding performance to our tools is the electrically controlled valve gate system. In the old days only hydraulic or pneumatic movement of the pin was a possibility, that is digital technology that only gives you the option of open or…
-
Gating for clear Polycarbonate
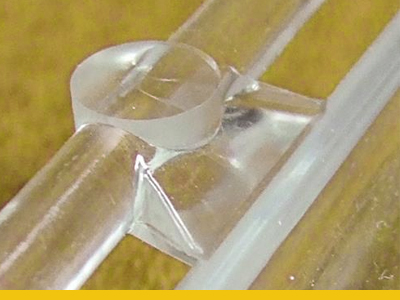
There are many factors to consider when you are trying to get a cosmetically correct part made from poly carbonate. For a toolmaker gating and venting are 2 of the most important. Gate: At The Tool Hub we recommend you to do all you can not to restrict the flow path. That includes: Increasing the…
-
Evaluate your gate balance
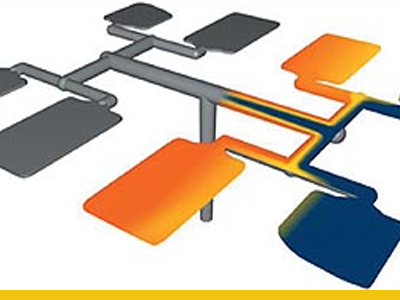
First step is to check the physical size of each gate through a dimensional report. Gates should always be made by using multiple rough and fine electrodes to ensure that the electrode wear will not cause any imbalance. We suggest never to spark more than 4 cavities with the same rough electrode, and to then…
-
2K – Design for success
Part and Mold Design for optimal 2K success. Part Design Basics •The wall thickness of the substrate and overmold should be as uniform as possible to obtain the best molding cycle time. Wall thicknesses ranging from 1.5 mm-3 mm will ensure good bonding in most overmolding applications. If the part requires the use of thick…
Contact : +44 1865 922550 / +46 31 30 88 200
/
e-mail : info@thetoolhub.com